Practical Guide · Manufacturing Improvement
CHOOSE & USE
OEE
Software
OEE Software (Overall Equipment Effectiveness) can support manufacturing improvement — but only if you use it right. Selecting the right software solution can make it grow, selecting the wrong one may block your road. Follow this framework to make the descision that fits best for you.
Foundation
What Is OEE & What is it value
OEE (Overall Equipment Effectiveness) is the gold-standard instrument for measuring manufacturing equipment effectiveness and visualizing where the losses are .
- A closed and balanced time study…
- …to reveal ALL effectiveness losses of a machine
- …by the shop floor team
- …to steer continuous improvement
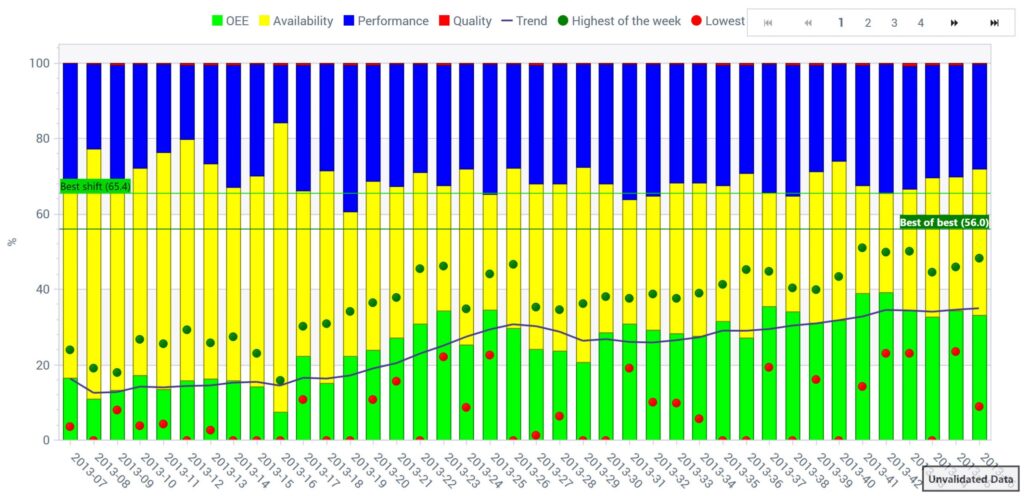
OEE comprises several KPIs
Multiple KPI’s
Besides Availability – Performance and Quality, OEE, as a tool for improvement, encompasses several KPI’s.
OOE
TEEP
Availability
OEE
TEEP
OEE has several time windows e.g.
- OEE: the schedule for regular shifts
- OOE: regular shifts plus excuded time
- TEEP: all potential time – 24/7
OEE softwrae selection
The 9-Step Selection Process
Rushing a software decision creates costly rework. Follow these nine steps to align stakeholders, define requirements, and validate your choice before committing.
There are different providers for different types of users. What type of user are you?
Inventory every machine, PLC, MES/ERP system, network segment, and existing dashboard. Document constraints such as legacy PLCs or intermittent connectivity that will shape your architecture.
The cost of OEE software and its implementation can range from a few to many thousands of euros.
The payback period can also vary considerably. What are your choices in this regard? Calculate the full TCO including training, support and upgrades.
There is a big difference between correct data and precise data; between a lot of data and the right data.
What requirements do you have for the data collected?
Do your OEE data need to be integrated into a wide range of other applications? And is this for just a handful of machines, or does the system need to be able to support dozens of factories?
Can any loss be revealed on any type of machine? Can you easily adjust this yourself? Is it possible to work with different types of shift schedules, etc., etc.?
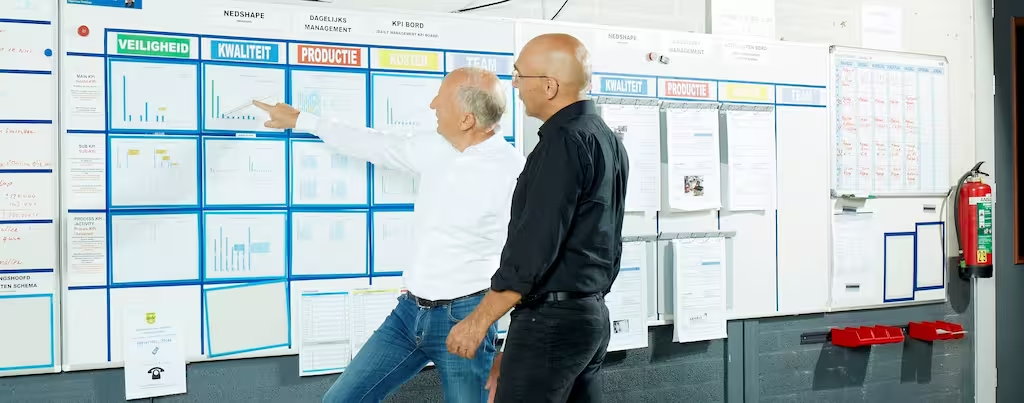
Who needs what sort of reports and analyses? What are your requirements for standardised analyses and reports? Who needs to be able to produce them, when, and how quickly?
Evaluate the UI. A solution rejected on the shop floor fails regardless of its features. Test the application’s speed. Long waiting times are a red flag in day-to-day use.
Does the supplier have production experience? Are they familiar with your sector, machinery and common problems? Do they have a proven track record of implementing improvements? Is there Proof of Value with measurable KPIs, review SLAs and roadmap alignment.
OEE software selection Checklist
The Selection CHECKLIST
When selecting suitable OEE software, there are many factors to consider, the importance of which you may only realise later on. To help you determine whether the software will meet your needs, you can use the questions below as a guideline.
Questions to help explore a solution
- How long does it take to get it technically running?
- How long does it take to configure it?
- Can it cope with the different situations/needs for definitions that I am facing?
- Does it support the OEE Industry Standard?
- How friendly is it to the user/operator? (check the need for training)
- Who’s solution will it be (is it IT owned, management owned or shopfloor owned)
- How deep are the possibilities to analyze losses? (Beware of overkill or even non-information, make sure it can provide what you need to improve your process)
- How are losses visualized, will the user easily understand this?
- How easy is quickly make reports/presentations?
- Does it generates the information you need when running a SGA/Kaizen event?
- What possibilities are there to visualize line/supply-chain issues?
- Does it also allow efficiency parameters to be monitored?
- Does it give sufficient feedback to operators (i.e. in case of errors or when interaction is needed?)
- How difficult is it to tap into machine signals?
- Can it be used for manual data-collection?
- Does it signals obvious data entry mistakes?
- What is the vision behind the product?
- Does it match with what you really want to achieve?
- Will the product be further developed? And how will that look like?
- Is your spokes-partner knowledgable about manufacturing and continuous improvement?
- Do you often hear “we can make that for you”? (Red Flag)
There are more points to consider, however those point hopefully lead you to the solutions that would fit your need. Feel free to ask my opinion; I will not sell you our software if that doesn’t fit with youe need because we only want to get positive reviews!
Good Luck, Arno

core pillars for improvement
3 oee core pillars
Software alone accomplishes nothing. For oee software to lead to real improvement, three core elements are required:
Set up your software so that all effectiveness losses are recorded and can be displayed.
Losses cost money: don’t allow them to remain hidden
Use OEE software to fight the invisible enemy.
Collecting the right data and being able to visualize losses in the right way requires effective software!
‘Organizing problems’, or eliminate them forever?
Good OEE software shows the way to turn information into improvement, leading to a fabulous ROI!
core pillars for improvement
8 steps oee implementation
A successful OEE software implementation requires more than just installing the software. By following these 8 steps, you will have put everything in place to ensure your OEE implementation is a success:
The goal: learn how it works and show a success
Implement OEE in the machine where success is guaranteed.
The next machines in line:
Implement OEE in machines where the focus of the improvement strategy must be directed. [More…]
define definitions for all the parameters within OEE in order to gain an overview on ALL hidden losses
In order to increase effectiveness:
- Do not accept the situation as long as it is not ideal.
- There are no excuses for not being ideal; there are merely causes of losses that must be eliminated! [More…]
involve the team in gathering the data: KISS – Keep It Short and Simple…
OEE registration will only gain support if the registration burden is acceptable
Keep in mind that OEE and OEE data collection is supposed to encourage the operator’s involvement and understanding! [More…]
Anyone involved by OEE, needs to have the right knowledge, attitude and skill.
It is not difficult, not a big thing, but crucial if you want everybody on board.
Unfortunately, all too often we see that everyone in the company has ample opportunities for training, yet no time is set aside for the production team to undergo essential training. It is the management’s job to make time for this!
After the first four steps you are ready to start:
the data can now be collected
Although collecting OEE data is just a small part of the OEE measurement, it usually gets a lot of attention. And unfortunately often in the wrong direction… Make sure to know the pitfalls! [More…]
After the data come in, they are of little use if they do not lead to the right response.
You will need to transform ‘data‘ into ‘information‘: Charts, reports etc.
The collected data must be processed before the next shift commences. Ideally, this is done by someone who is closely involved with the process but who still has an overview of the various process steps, such as a line manager or department manager. [More…]
At latest before the next shift, the team should receive the information they need to respond to.
Without a fast and correct feedback loop, you will miss the desired change of behavior.
OEE is primarily a ‘shop floor tool’ for creating awareness, focus and ‘ownership’.
This is what it is all about: Helping the production team gain insight into the existing losses. [More…]
Management needs relevant information to provide the means that are needed to improve the demonstrated situation.
The team provides this information and expects the support of the leaders.
The role of the management in OEE is to manage improvements in the organization. The production team can help by supplying management with the right information. [More…]
RISK PREVENTION
Common Pitfalls to Avoid
01
THE ILLUSION OF BEING IN CONTROL
REAL TIME OEE
Responding to every incident is known as ‘micromanagement’. This rarely leads to improvement and certainly not to growth.
02
THE ILLUSION OF COMPARING
BENCHMARKING
Comparing OEE figures is impossible for a number of reasons. Comparing apples with oranges leads to incorrect conclusions and decisions.
03
THE ILLUSION OF KNOWING IT
EXCLUDE SHOPFLOOR
If you think the production team can do nothing but produce, you are stifling your greatest potential for improvement
04
HEAD-IN-THE-SAND POLITICS
HIDING LOSSES
By hiding all sorts of inefficiencies from your OEE, your OEE figure may improve, but of course your actual effectiveness will not. It’s a case of burying your head in the sand!
05
THE ILLUSION OF PRECISION
FULLY AUTOMATED
‘Precise data’ obtained through fully automated data collection does not automatically result in accurate data or meaningful information.
06
THE ILLUSION OF IMPROVEMENT
MEASURE EVERYTING
Measuring every machine does not automatically lead to improvements across all of them. Measuring everything is not the same as improving everything.
Ready to start your OEE journey?
Whether you want to generate profit or gain control, we’re happy to help you get started!